Fin Dies
Fin Die 5mm
Contact for quote
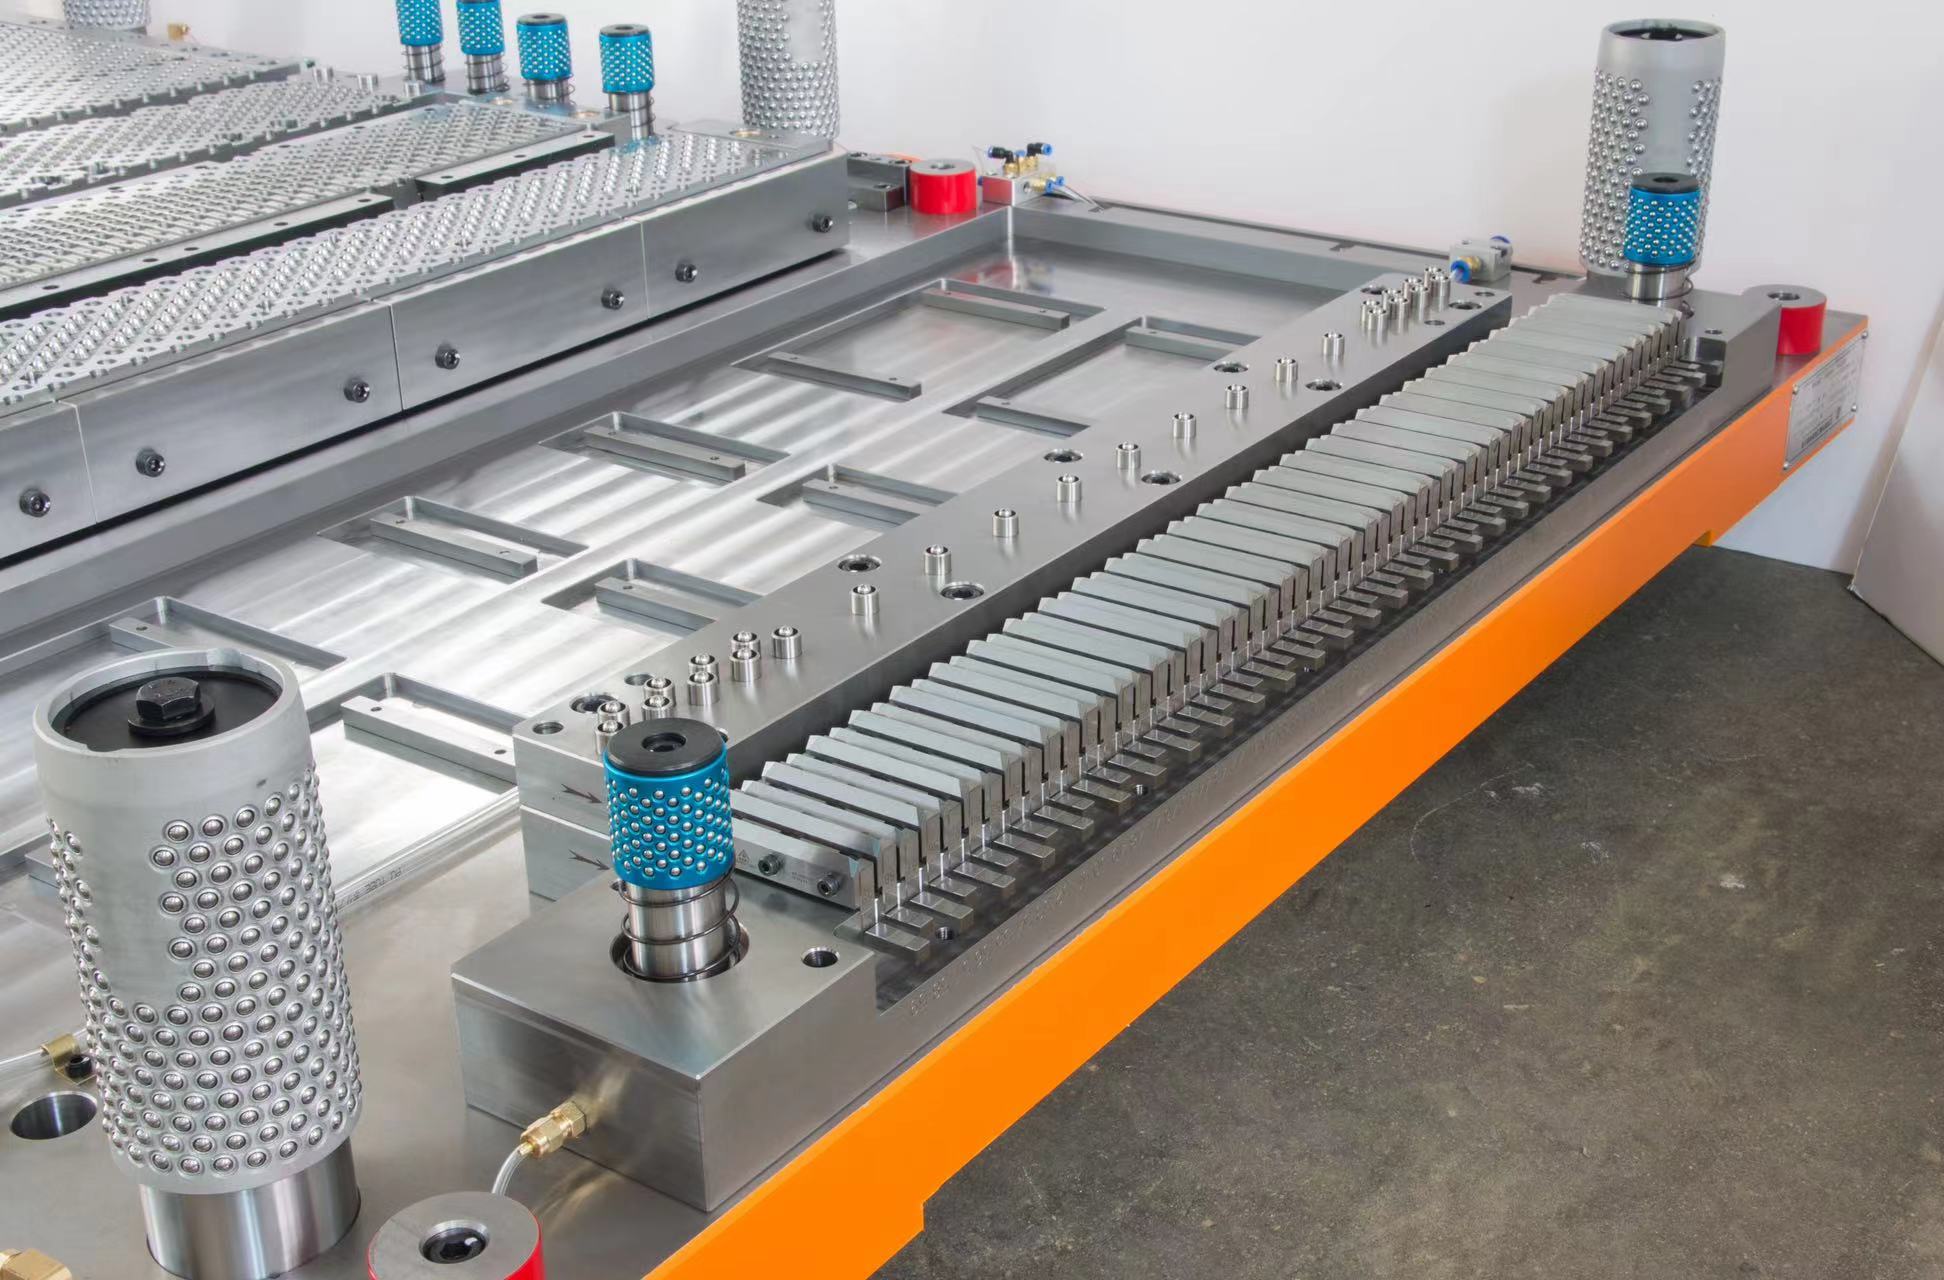
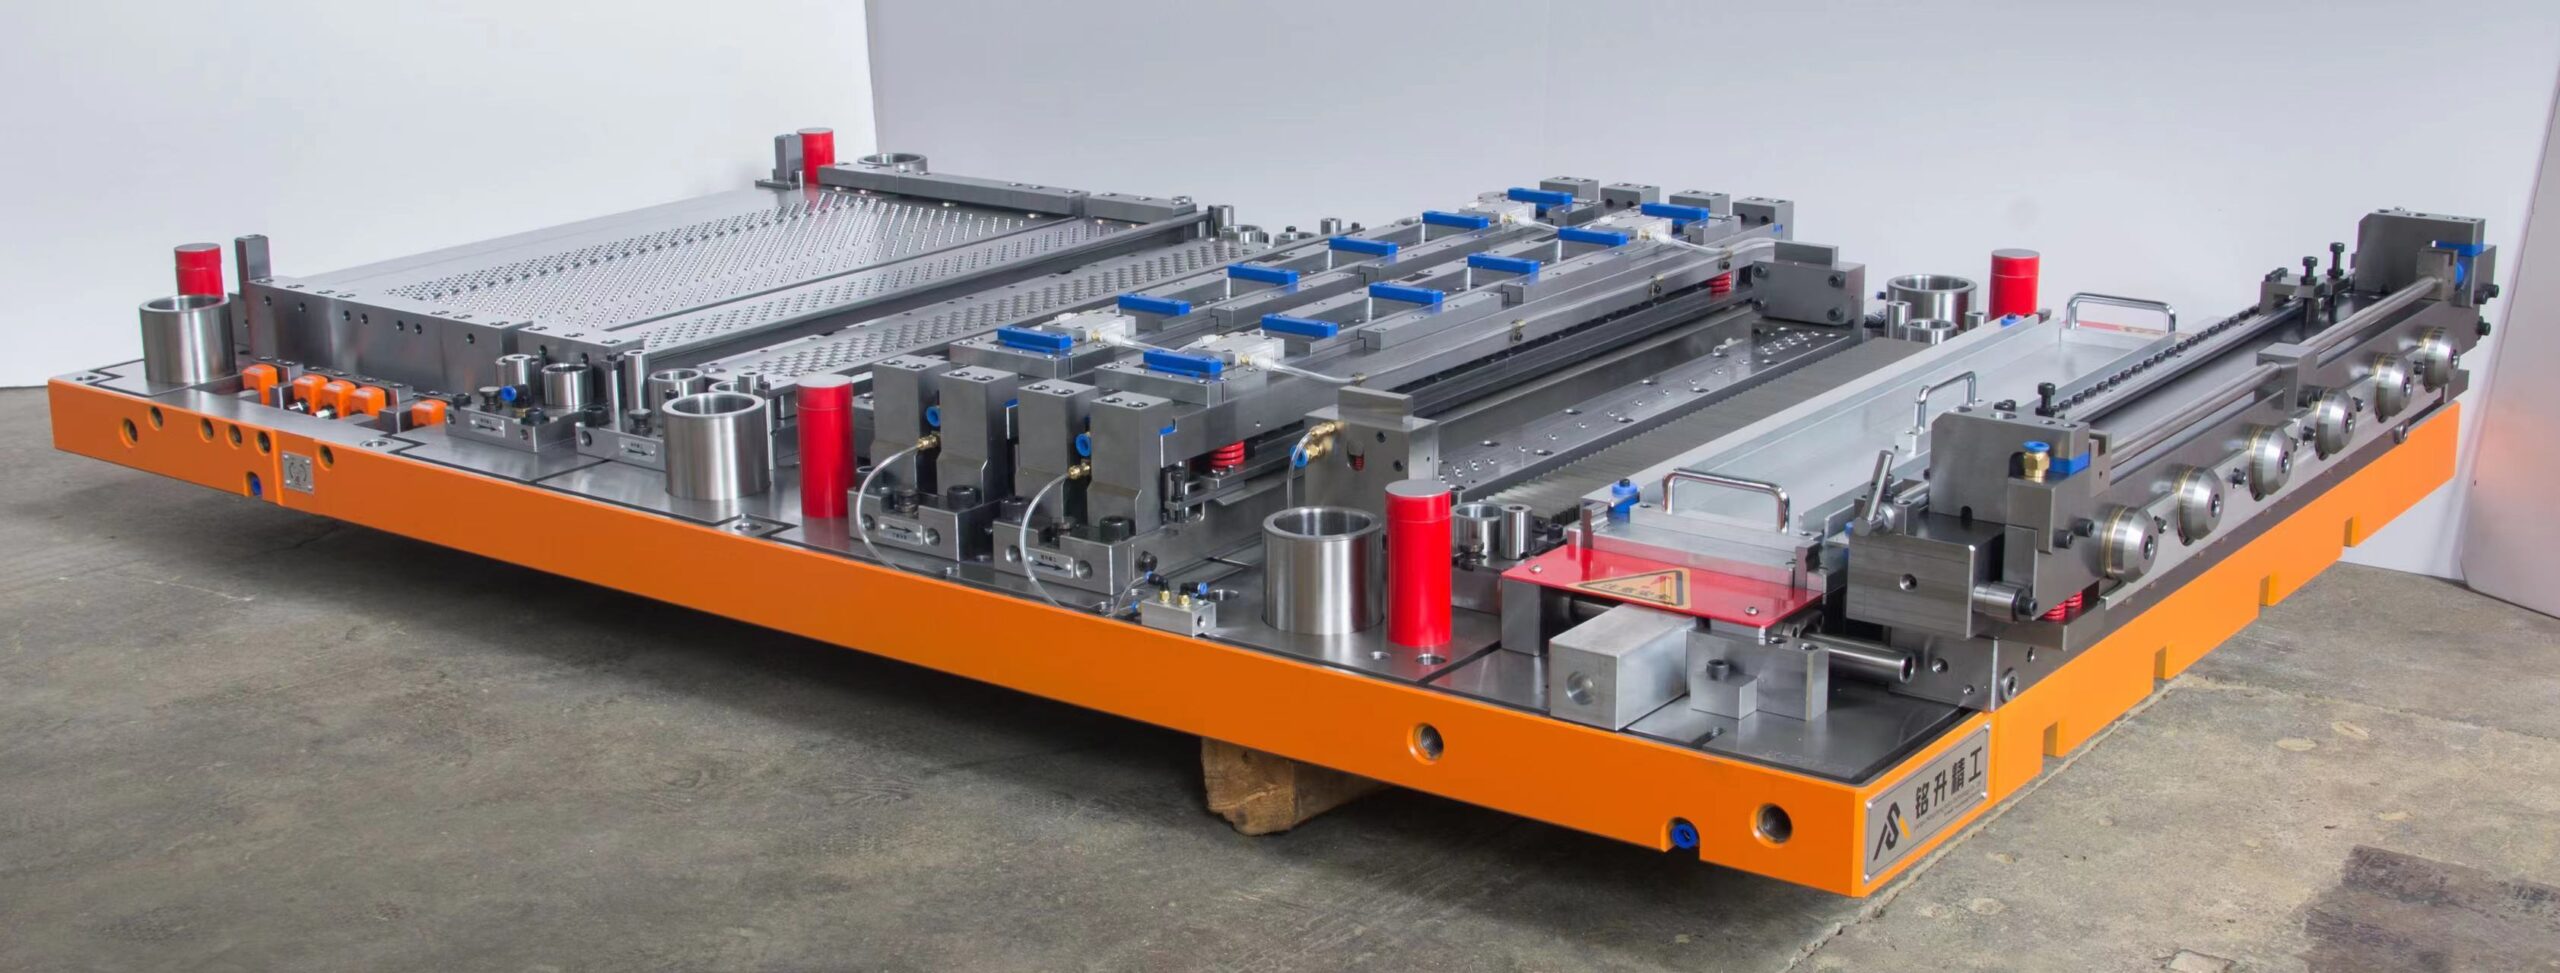
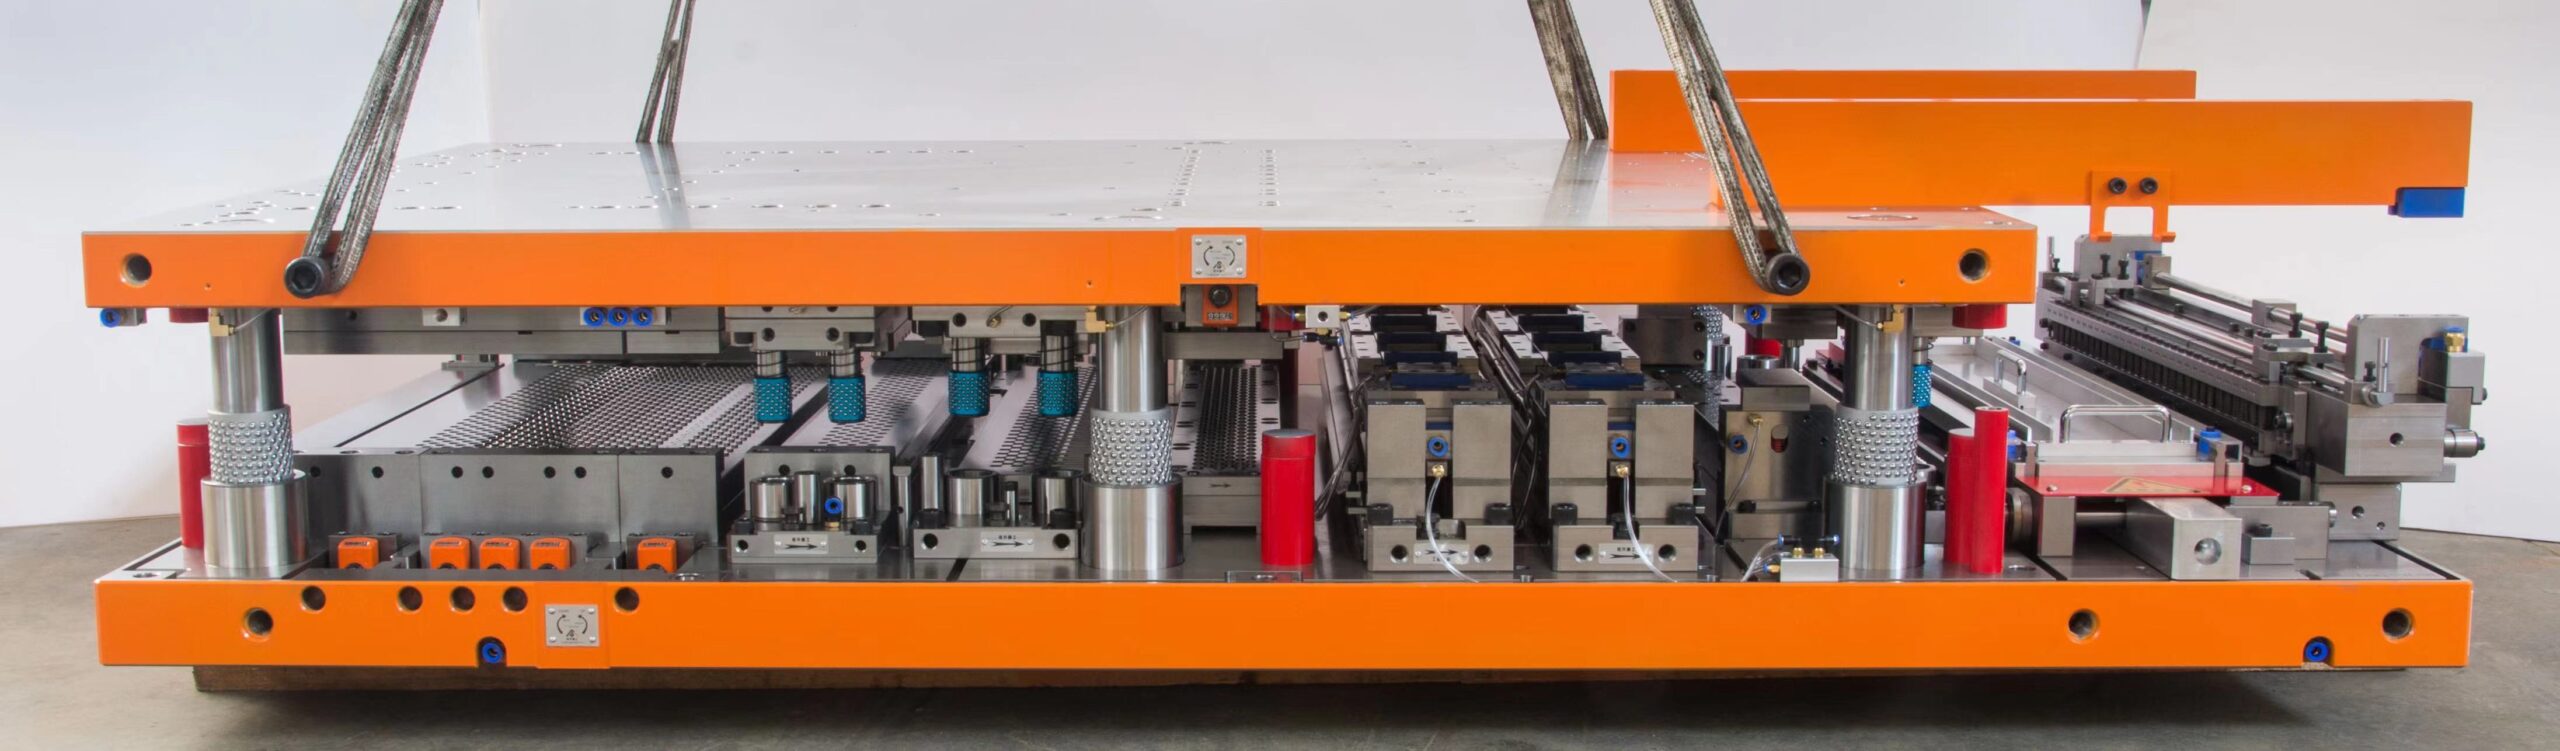
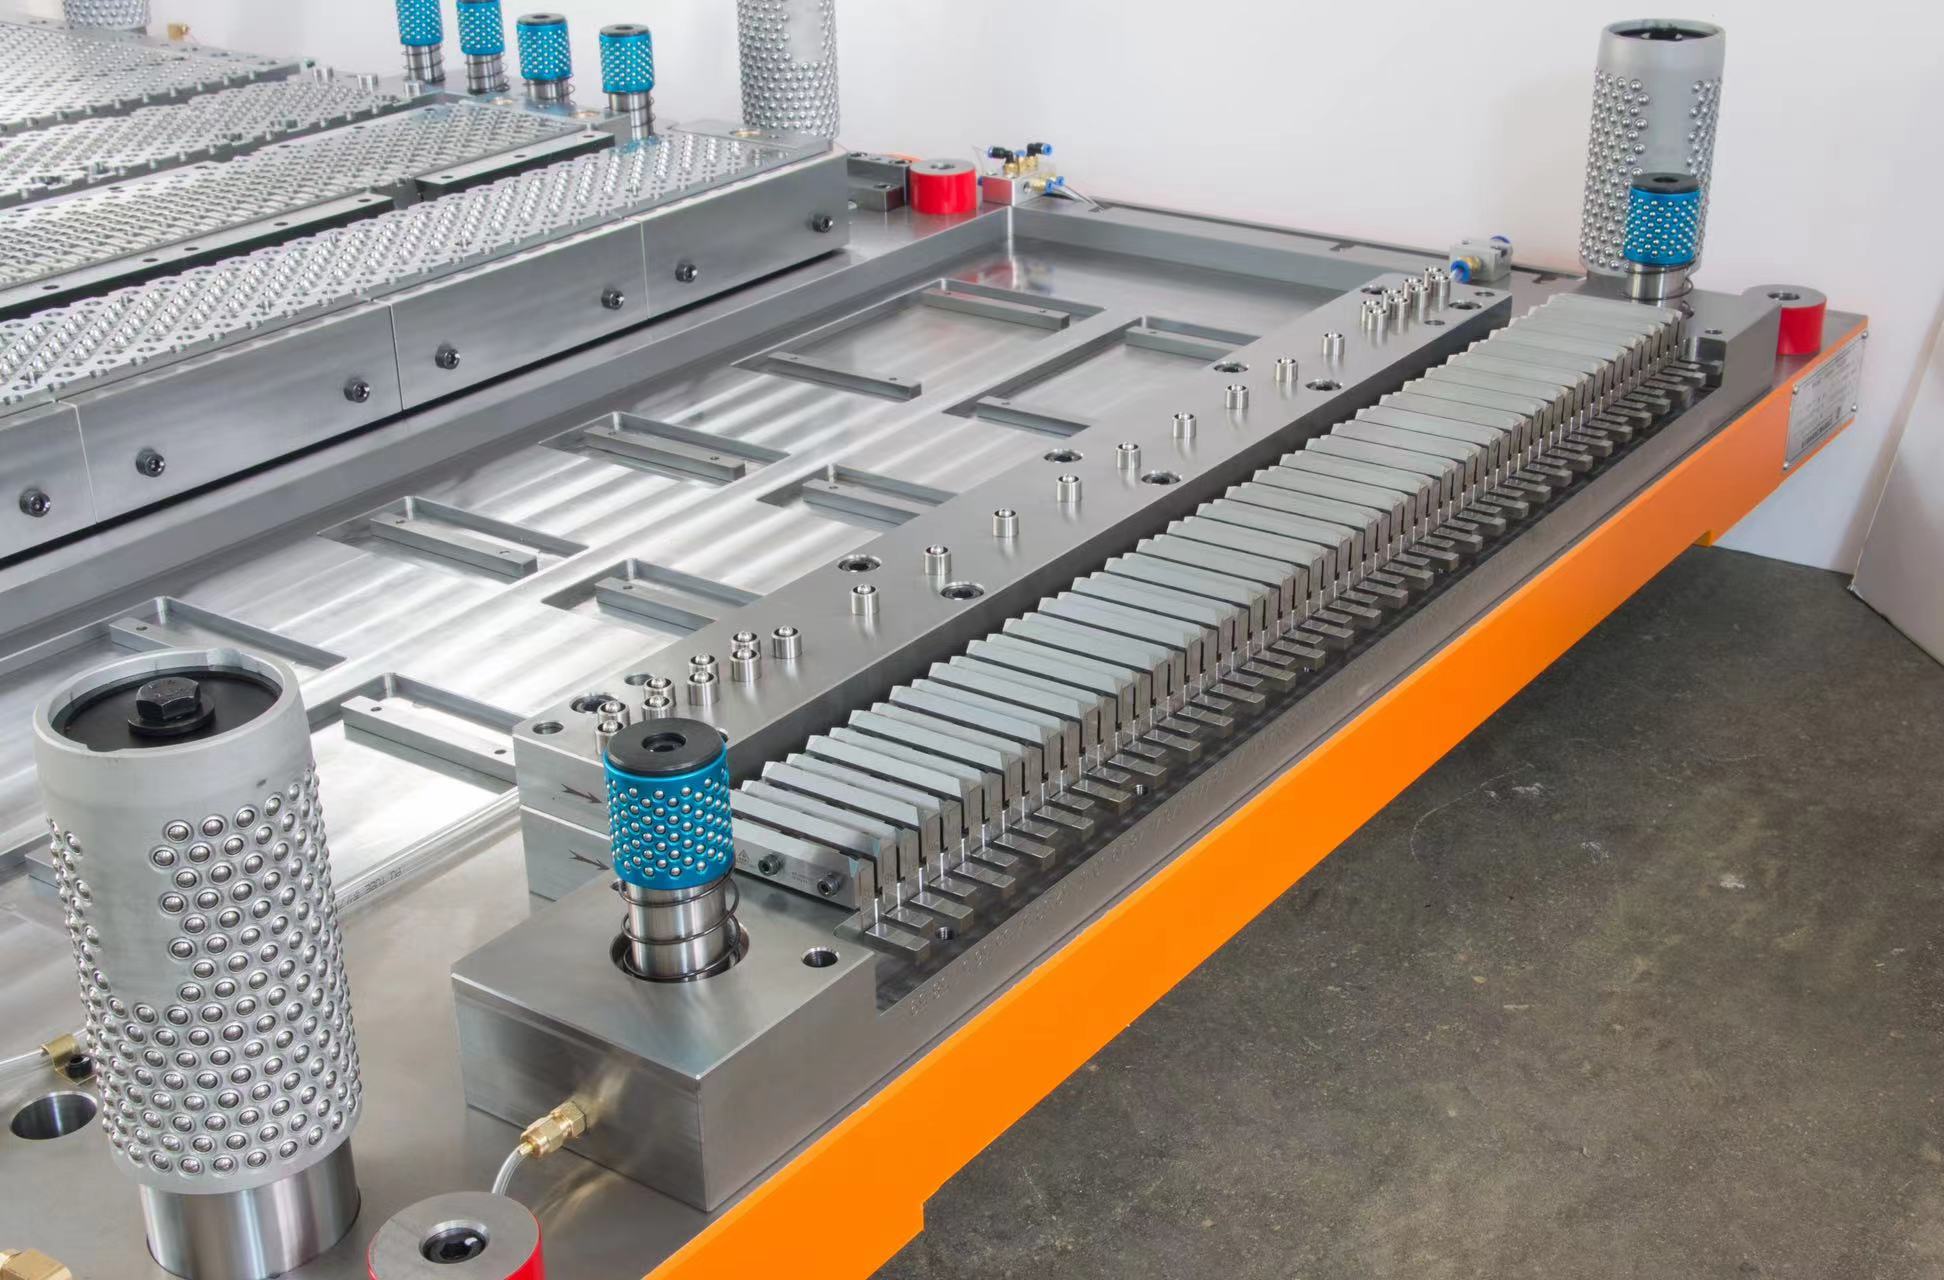
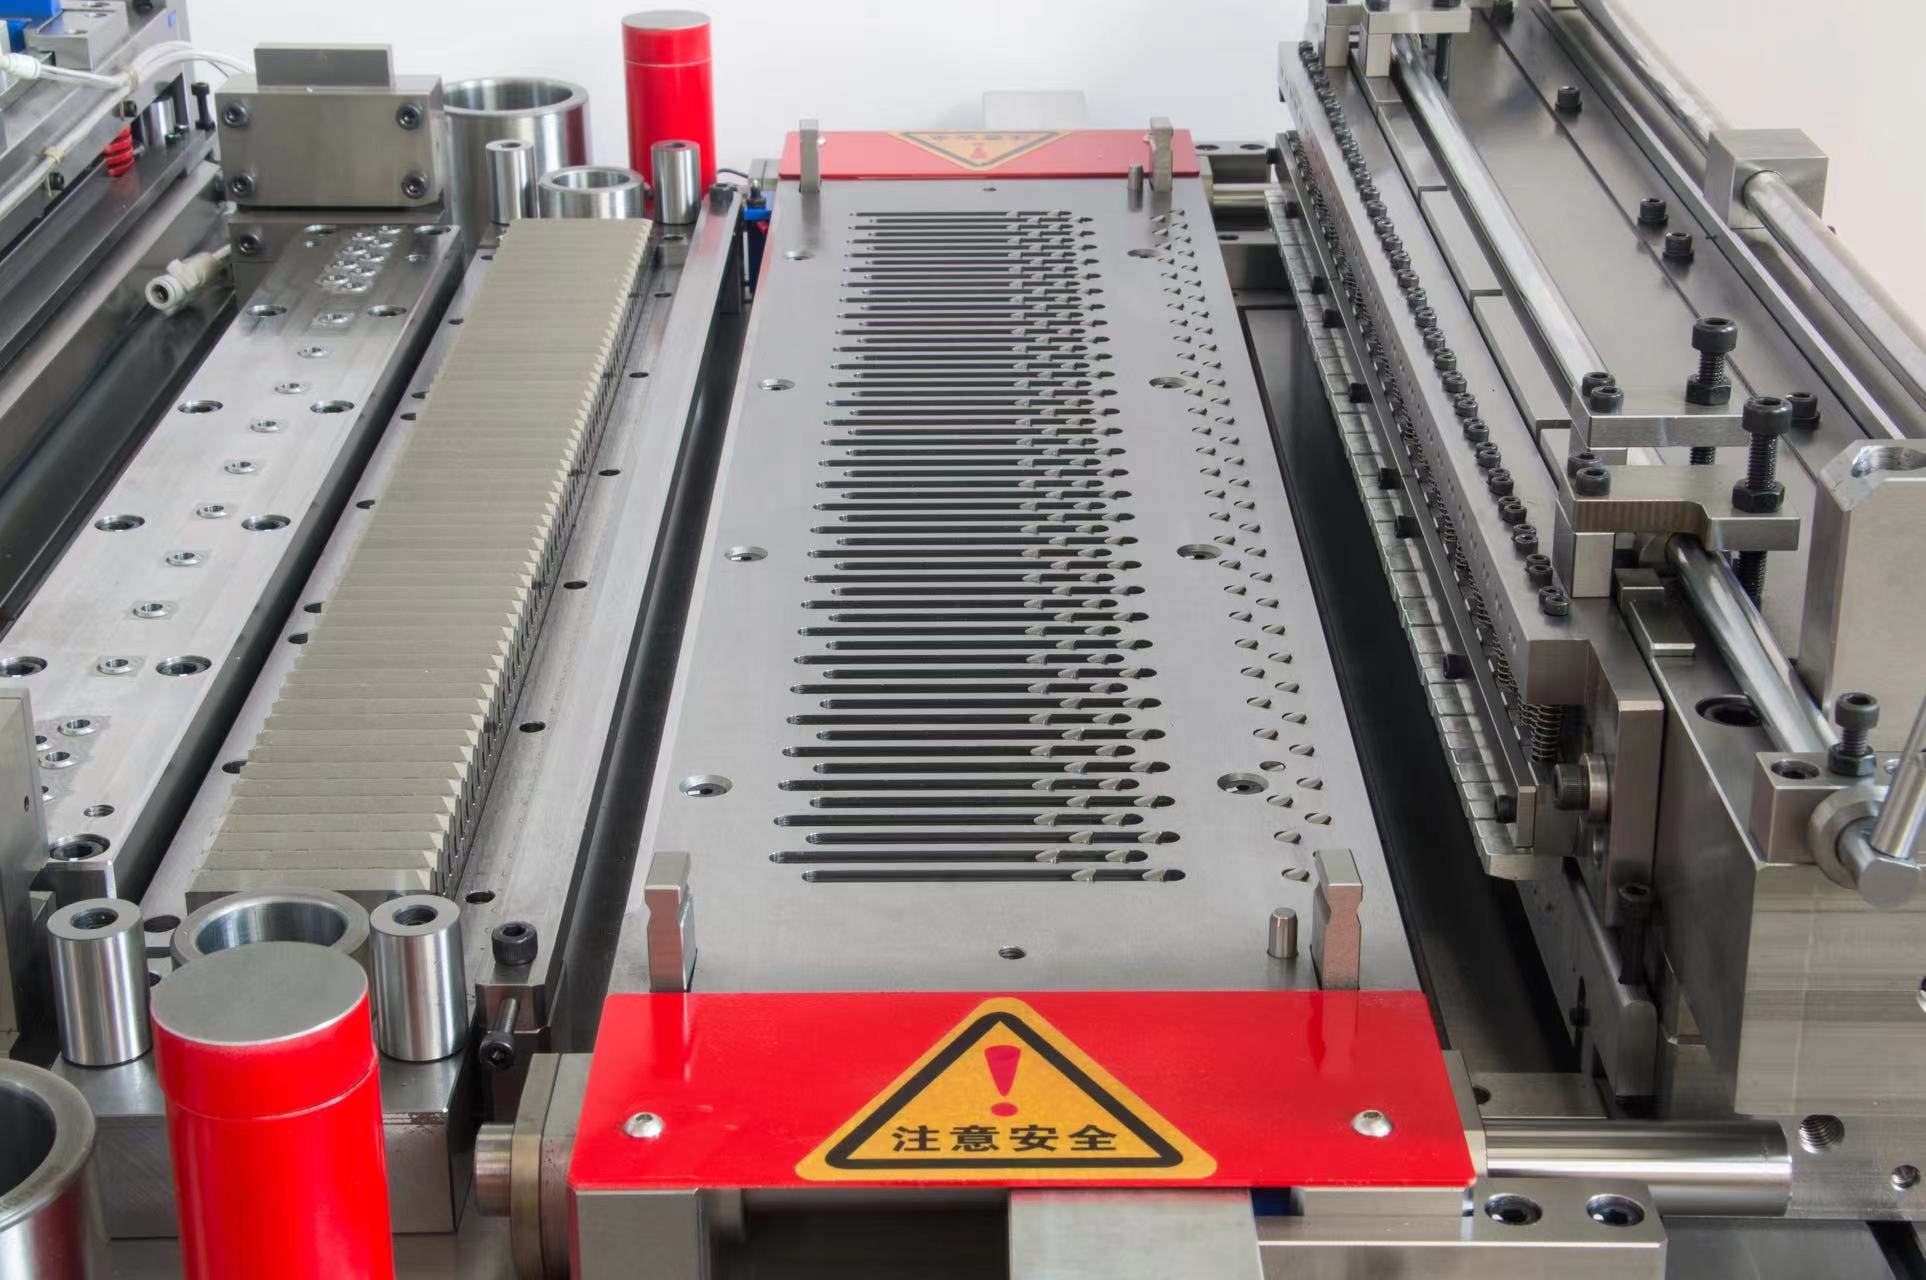
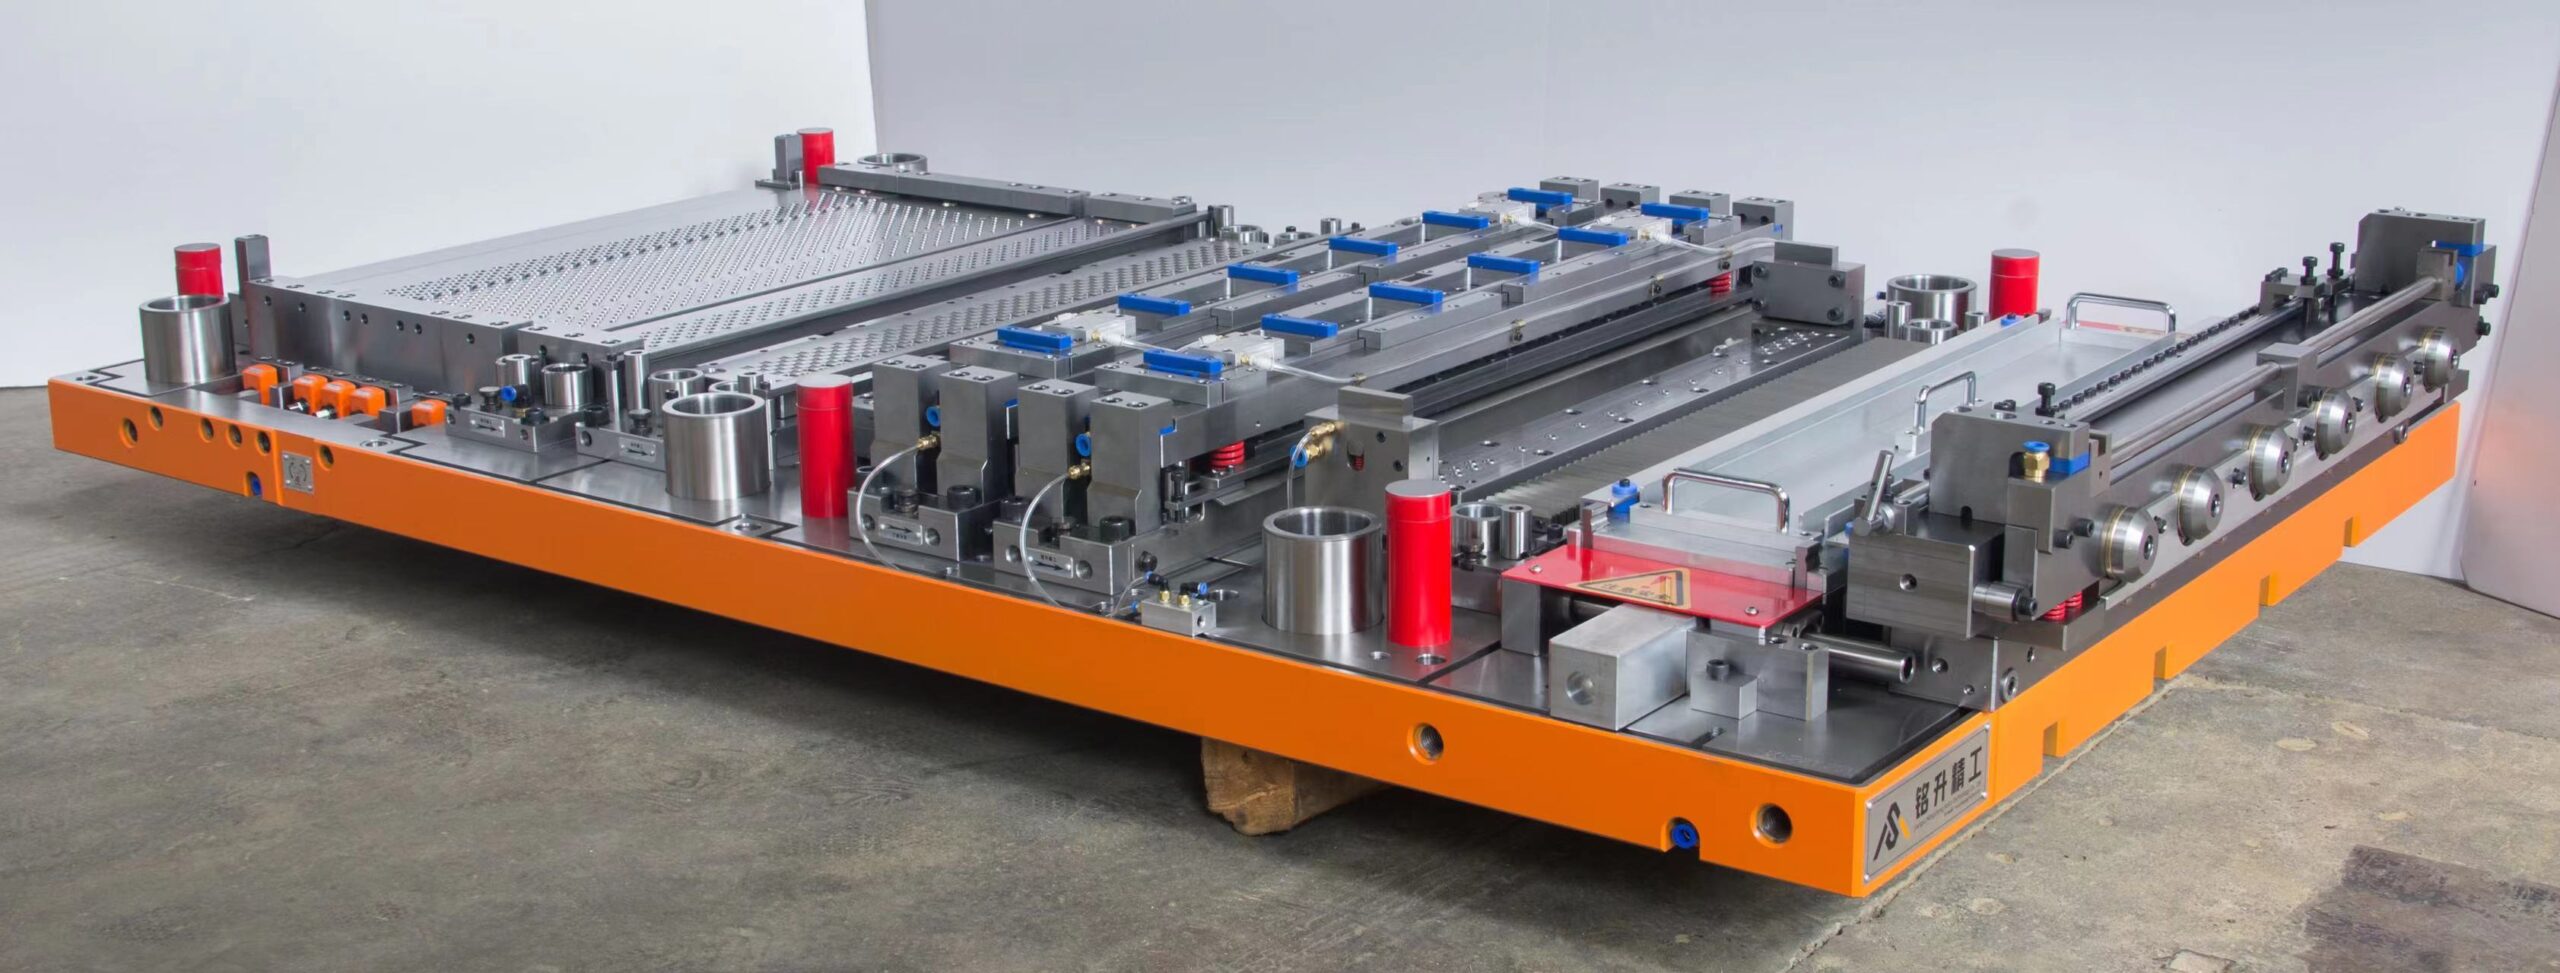
A Φ5.2×24R×2P progressive fin stamping die with a lance-forming station — staggered, plain-surface fins for compact HVAC and refrigeration heat exchangers.
Progressive fin stamping die, model Φ5.2mm×24R×2P, built for an AK85 open-type fin press (Aomate, Ningbo).
Fin specification: 19.05mm hole pitch within a row, 11.60mm width (single row), Φ5.20mm ±0.05mm fin hole, staggered pattern, plain fin surface, stamped in continuous strips of 4 to 52 holes per fin length.
Compatible material: China-representative O-temper or H22 hydrophilic aluminum foil (elongation >20%), 0.11mm thick, 289mm stock width. Collar height is adjustable from 1.4mm to 1.9mm at this thickness.
Punching process (10 stages): Drawing → Piercing/Extruding and Drawing → Lance → Re-flaring → Notching 1 → Notching 2 → Edge trimming → Row slitting → Feeding → Straight cut-off.
1. Drawing — completed in multiple steps, each independently height-adjusted via a SIKO regulator on the die.
2. Piercing/extruding and drawing — punching completes first as the press slide descends, then drawing finishes on the same stroke. The piercing sub-die uses an independent guide-post/guide-bush structure for forming precision and long service life; punch-to-die concentricity is held within 0.002mm for full interchangeability. Punches are air-purged in both directions with automatic mist lubrication for forced scrap discharge.
3. Lance — forms the lance (bridge) profile on the fin surface.
4. Re-flaring — collar height adjusts arbitrarily via the same SIKO regulator.
5–6. Notching 1 and 2 — cut the custom notch shapes called for on the fin drawing.
7. Edge trimming — an independent structure trims excess edge material with a slug-retention feature to maximize cutting-edge life.
8. Row slitting — upper and lower blades cut 1 to 6 rows of fins in a pop-up, quick-switch cartridge; the upper plate is engraved 1–23 across for fast row-count changes, with a controlled blade gap for clean, burr-free strips.
9. Feeding — a pull-type feed uses fine grippers seated in the formed holes, driven by a connecting rod between die and press; feeding fingers are SKD11 tool steel for accurate long-run, high-speed positioning.
10. Straight cut-off — length-wise cutoff via cylinder, solenoid valve and the press's electrical control, with oil-free lubrication at the cut face; an independent adjustment sets each row's fin curvature, and cut-off position can shift half a pitch for precise, collision-free hole alignment.
Build quality: piercing punch/die, row-cutting, edge-trim and cut-off blades are ASP30 tool steel from Sweden at HRC62–64; the lance cutters are ASP30 at HRC60–62. Upper/lower plates are P20 pre-hardened steel (China); the station set, punch/die fixing plate and stripper are PDS5 pre-hardened steel (Japan).
Quality assurance: 12-month warranty from delivery, with lifetime paid maintenance available. Punching parts are guaranteed for 25 million+ strokes on aluminum foil before resharpening, with up to 10 regrinds over the die's service life. Normal working speed is 150–210 SPM.
Request a Quote for This ItemTechnical Specifications
| Die Model | Φ5.2 × 24R × 2P (progressive) |
|---|---|
| Compatible Press | AK85, open-type (Aomate, Ningbo) |
| Fin Hole Diameter | Φ5.20mm ±0.05mm |
| Hole Pitch (Same Row) | 19.05mm |
| Row Width | 11.60mm (single row) |
| Hole Pattern | Staggered |
| Fin Surface | Plain, with lance-formed bridge feature |
| Stamping Range | 4–52 holes per fin length |
| Working Speed | 150–210 SPM |
| Compatible Material | O-temper/H22 hydrophilic aluminum foil, 0.11mm × 289mm |
| Collar Height (Adjustable) | 1.4mm – 1.9mm |
| Row Cutting Columns | 1–6 (up to 23-column plate) |
| Wear Part Steel | ASP30 (Sweden), HRC62–64 |
| Warranty | 12 months + lifetime paid maintenance |
| Punch Durability | 25,000,000+ strokes before resharpening |
More from Fin Dies
fin dies
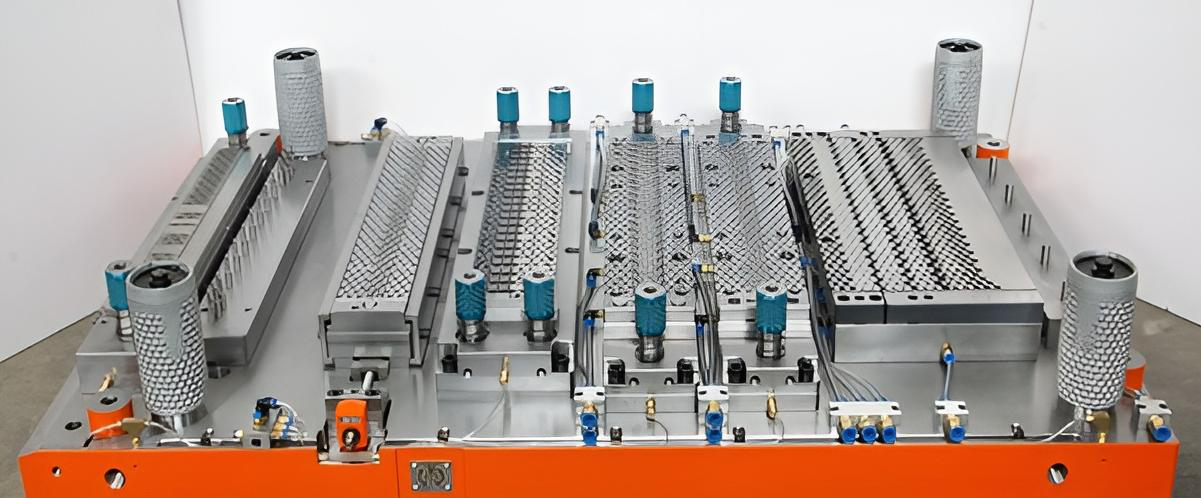
Fin Stamping Dies (4mm–25mm)
Custom progressive fin stamping dies for tube diameters from 4mm to 25mm, in aluminum, copper, aluminum-magnesium alloy or stainless steel — built to match American, Italian, Japanese or Chinese press styles.
fin dies
7mm fin die
A Φ7.3×24R×2P progressive fin stamping die with a louver-forming station — staggered, plain-surface fins for HVAC and refrigeration heat exchangers.
fin dies
12.7mm Fin Die
A Φ12.7×8R×1P progressive fin stamping die that pierces heat-pipe holes alongside the main fin holes — staggered, V-corrugated fins for HVAC and refrigeration heat exchangers.
Get a Quote